personalized metal leaf petal flower wall mirrors maker - Bulk Supply and Specification Guide
What This Product Is and Where It Fits
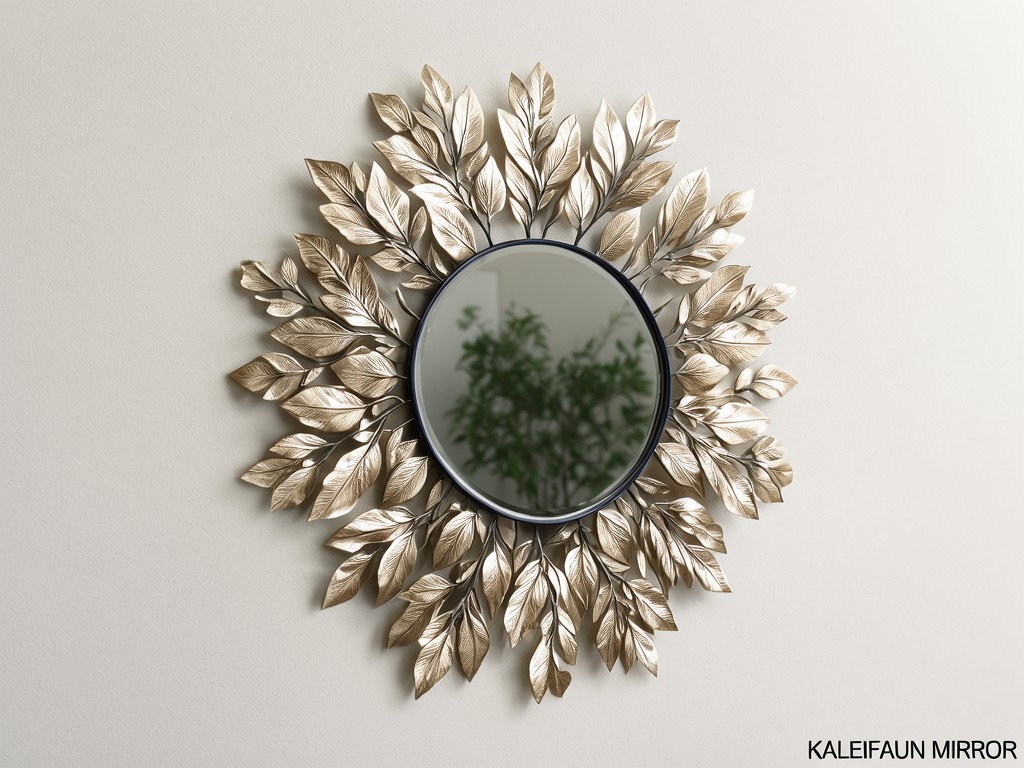
A metal leaf-petal flower wall mirror combines a central mirror with a decorative surround formed from shaped metal leaves or petals. For private-label ranges, the design is usually built around a cut or stamped steel frame, a coated finish and a mirror glass panel secured to a rear support. The product is sold as decorative wall décor, where visual symmetry, secure hanging and safe arrival matter as much as the appearance in a product image.
Personalization can cover the overall diameter, petal profile, finish colour, mirror size, rear hanging hardware and retail packaging. Keeping those choices tied to an approved drawing and sample helps a buyer repeat the same look across replenishment orders instead of re-approving a subtly changed silhouette or finish.
Where Cheaper Alternatives Fall Short
Low unit price can conceal variation at the points customers notice first. Uneven petal spacing makes the flower appear off-centre; thin metal can flex during handling; and inconsistent weld placement may leave one section sitting proud of the wall. If the mirror is not adequately supported, transport vibration can loosen its fixing or create edge pressure that leads to cracks.
Finish shortcuts also show up after sale. Poor surface preparation can cause coating chips around cut edges or welds, while an uneven coating can soften the detail in narrow petal gaps. Those defects create returns, replacement freight and negative reviews. A lower purchase price only helps total cost when the construction and packing keep these failure points within the buyer’s approved limits.
Measured Performance in Real Use
Balance and load analysis shows whether the wall hardware and rear support suit the finished mirror’s actual mass, not just its outer diameter. A larger metal surround shifts more weight away from the wall fixing, so the hanger position and attachment method should be checked against the completed unit. Buyers should approve the intended wall-mounting arrangement and specify any wall anchors separately when the product is sold for different wall types.
Set measurable limits on overall diameter, mirror opening, finished weight, petal alignment and hanger position in the approved specification. A defined tolerance for each feature gives production and incoming inspection a shared basis for accepting repeat batches.
Reflected-image checks matter too. A mirror can pass a basic visual review yet show noticeable distortion if the glass is unevenly supported or pressed at its edges. The approved sample should establish the acceptable reflection, glass edge condition and finished appearance, with checks performed on units from the production run rather than on a display sample alone.
Comparing Two Standard Configurations
The interface between parts determines how much assembly control and protective packing a design needs. Use this selection path to match construction to the price point and expected handling:
- Start with the surround. Stamped steel petals suit repeat designs with consistent shapes and a controlled tooling cost; choose this route when the artwork can stay stable across orders.
- If the outline includes custom curves or varied leaf shapes, use individually cut metal pieces. This adds cutting and assembly work, but supports more distinctive profiles without committing to a dedicated stamping die.
- Then choose the finish. Powder coating gives a consistent colour layer across the surround and is suited to standard retail finishes; confirm colour against a physical approval sample because screen values do not define the final appearance.
- For a metallic look, select a plated or other specified surface treatment only after reviewing the sample and its edge coverage. Extra finishing steps can raise unit cost and create another source of batch variation, so include visible edges and recesses in the approval criteria.
The lowest-cost route is not automatically the lowest-cost program. Tooling amortization, manual assembly time, protective materials and the risk of finish or alignment returns all affect landed cost across a repeat order.
How Consistency Is Held Across Batches
Consistency depends on controlling the drawing, sample and production references as one specification. Record the material thickness, petal count and profile, joining locations, mirror dimensions, coating colour, hanger position and finished weight against the approved version. A change to any of these details should be reviewed before production, since even a small adjustment can alter the mirror’s visual balance or packing fit.
Batch checks should compare samples from the start, middle and end of production. That approach helps identify drift in colour, spacing or assembly before cartons are closed. For private-label orders, retain the approved artwork and reference sample with the order record, and link carton labels to the production batch so a reported defect can be traced to its shipment.
Packaging is part of repeatability, not an afterthought. Specify how the mirror face, projecting petals and hanger are protected, then approve the packed configuration before the first bulk shipment.
| Packaging item | Specification to confirm | Batch-control purpose |
|---|---|---|
| Mirror-face protection | Protective film or face cover, plus a non-abrasive contact layer | Reduces surface marks from contact during packing and transit |
| Petal and edge protection | Formed inserts or guards that prevent metal-to-glass contact and petal deformation | Limits coating chips, bent details and pressure on the mirror edge |
| Retail and master carton | Approved artwork, product identification, carton quantity and batch reference | Supports receiving checks, stock control and defect traceability |
Inspection Items and Test Methods
Incoming metal should be checked against the agreed thickness and finish requirements. During fabrication, verify overall dimensions, petal spacing, joint placement and the stability of the rear support. A visual check under consistent lighting can identify coating skips, scratches, sharp edges and visible weld defects; dimensional gauges or a controlled measuring fixture make repeat checks less dependent on operator judgement.
After assembly, check mirror size, edge condition, face cleanliness, reflection and hanger alignment. Apply a controlled load to the wall-hanging point on representative units using the buyer-approved procedure, then inspect the attachment and surrounding frame for movement or damage. The test load and acceptance criteria should be agreed for the design rather than assumed from the product category.
Inspect coating adhesion and coverage on sample pieces, with attention to cut edges, recesses and welded areas. For transit validation, pack a production-representative mirror in its final retail configuration and assess the carton and product after the agreed handling sequence. Record defects by type and batch; repeated damage at the same contact point calls for a packaging or assembly correction before the next order.
Project Discussion
Share your target dimensions, reference artwork, preferred metal finish, mirror specification, order quantity and destination packaging requirements. A review of these inputs can establish a controlled sample and inspection plan before a repeat batch is priced.
Discuss a private-label specification and batch-control requirements with the production team through a project inquiry.