Customized modern ornate oval wall mirror China factory: Specification, Ordering and Quality Notes
Construction Method and Its Effect on Consistency
First-article tooling determines how closely ornate frame details repeat from one production batch to the next.
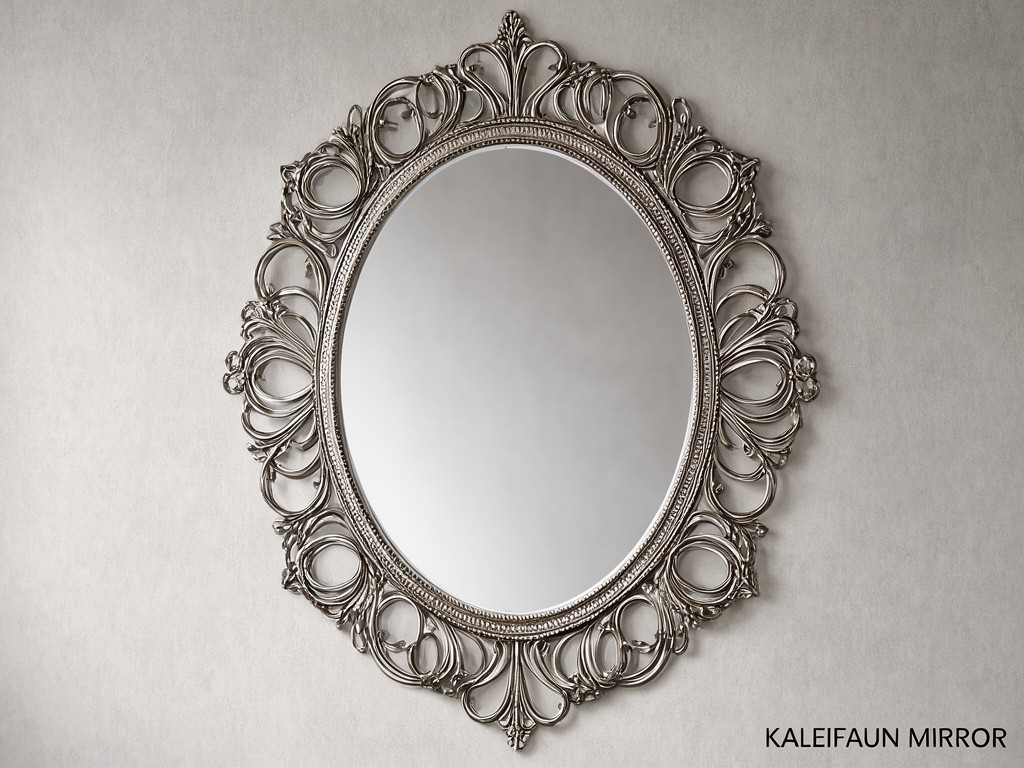
A typical build pairs oval mirror glass with a molded polyurethane frame, a prepared backing, and wall-hanging hardware. The frame master pattern and mold establish the relief depth, outer profile, and join lines; the glass is cut to the approved oval dimensions, its edge is ground, and the backing is applied before assembly. Paint, metallic leaf, or other surface finishes add separate process steps, so the approved finish sample should be signed off before the production schedule is fixed. For repeat orders, retaining the approved mold and finish reference reduces variation and avoids a new tooling review.
| Frame Route | Detail and Repeatability | Cost and Scheduling Effect |
|---|---|---|
| Molded polyurethane | Suitable for repeated relief details and a consistent oval frame profile after the mold is approved. | Requires upfront mold cost; larger repeat volumes spread that cost across more units and can shorten repeat-order preparation. |
| Carved timber | Allows a carved appearance and visible wood character, with more hand-finishing variation between pieces. | Can limit dedicated mold expenditure, but labor and timber selection can raise unit cost and extend batch preparation. |
Size, Weight and Specification Range
Consistency is set at the forming stage, then checked against the glass and assembled frame.
Common project dimensions run from about 400 × 600 mm to 800 × 1200 mm, measured at the frame’s outer edge; custom proportions can be quoted from a drawing. Mirror glass is often 3–5 mm thick, subject to overall size, frame support, and the buyer’s handling requirements. Finished weight depends on glass area, frame material, backing, and hardware, so approve a complete sample for carton and wall-fixing decisions rather than estimating from glass thickness alone.
Specification rule: confirm outer frame dimensions, visible glass opening, glass thickness, hanging orientation, and hardware position on one controlled drawing. A change to the frame profile can alter the glass opening and packed dimensions even when the overall oval size stays fixed.
OEM and ODM Programme Structure
Process choice shows up later as tooling ownership, surface repeatability, and the amount of artwork revision needed before a launch order.
For OEM work, buyers supply the approved dimensions, frame reference, finish target, logo or retail label files, and packing requirements. ODM development can start from a sketch or reference image, followed by a profile drawing, mold review, finish sample, and complete pre-production mirror. New ornate relief generally needs dedicated tooling; a simpler change to paint color or label artwork usually does not. Quote tooling separately from the per-unit price so the cost can be compared across an opening order and planned reorders.
For launch-date control, reserve time for drawing approval and sample transit as well as factory production. Changes after mold approval can require a revised sample and may move the order slot.
Quality Control and Batch Consistency
Mirror complaints often begin at the interface between glass, frame, finish, and hanging hardware. A repeatable inspection plan checks each of those areas against the approved sample and drawing, with batch records tied to the order and finish reference.
| Use or Handling Condition | Likely Complaint | Specification or Check to Set |
|---|---|---|
| Retail display under consistent store lighting | Visible finish shade or gloss differences across units | Approve a physical finish sample and inspect color, gloss, and coverage under agreed lighting conditions. |
| Repeated lifting and rehanging by end users | Loose hanger, shifting hardware, or frame separation | Specify hardware position and fastener type; check attachment and frame-to-backing fit on assembled samples. |
| Long-distance freight with stacked cartons | Chipped glass edge, cracked frame detail, or scuffed finish | Set edge protection, frame clearance, and carton orientation; assess a packed sample before shipment approval. |
| Routine indoor use in a humid room | Backing deterioration or finish damage near exposed edges | Review the mirror backing and edge coverage for the intended room conditions; include edge and backing inspection in batch checks. |
Dimensional checks should cover the outer oval, glass opening, and hanger location. Visual inspection should also look for scratches, distortion, bubbles or gaps in the finish, and damage to the molded relief; the buyer and factory can record acceptance limits on the approved sample.
Volume Planning and Lead Time
Tooling cost and production timing depend on how much of the frame design is new.
A new mold adds development time and a one-time charge before regular production; higher order quantities spread that charge across more pieces and can improve the unit price. They may also require a longer production slot, more packing materials, and earlier booking of freight. A finish change on an existing frame can have a lower setup burden, but small batches may still carry a higher unit cost because setup and inspection effort are divided across fewer mirrors.
As a planning guide, allow roughly 2–4 weeks for new tooling and sample approval, then about 30–45 days for production after sign-off. These are working estimates, not shipment promises: mold revisions, finish matching, glass availability, order volume, and export packing can change the schedule. Confirm the factory’s current slot against the required ship date before committing to a retail launch.
For a tooling review, send the target outer dimensions, reference artwork or image, desired finish, order quantity, destination, and required ship window. Discuss the mirror specification and schedule before the sample and production dates are locked.