Customized Decorative Sunburst Wall Mirror Factory - Bulk Supply and Specification Guide
Material choice starts with the conditions the mirror will meet. For a sunburst design, the central glass, radial frame and surface finish all affect cost, appearance and handling: thin formed steel can support a fine spoke profile, while a heavier metal section adds mass and can increase freight and wall-fixing demands. Glass thickness and the way it is retained also affect the finished depth and the space available behind the frame.
Indoor placement is the usual basis for specification, but sunlight through a window, frequent dusting and household cleaners can change how a finish looks over time. Chlorine vapour, sweat and abrasive pads are not routine mirror-cleaning conditions; for spa or hospitality projects, specify the actual exposure before choosing a coating or plated finish. Early approval of a physical sample gives OEM and wholesale buyers a firmer reference for production and launch scheduling.
Construction Method and Its Effect on Consistency
A common production route uses a stamped or laser-cut metal hub, formed radial pieces and a central mirror secured to a backing or retaining assembly. A locating jig keeps spoke spacing and the circular outline consistent during joining. Laser cutting suits lower-volume designs or frequent artwork changes; stamping becomes more cost-effective when the design and order quantity justify dedicated tooling.
Joining heat can pull a thin frame out of plane, while uneven forming can make the rays look crowded on one side. The factory checks the assembly against a centreline and diameter reference before finishing. Deburring and surface preparation matter too: rough edges can show through a coating, and residue can interfere with finish adhesion.
For repeat orders, approve the spoke layout, frame depth, finish sample and mirror-retention method together. Changing one after tooling or sample approval can affect fit, appearance and the production schedule.
Specification Range and Customisation Limits
Dimensions below are starting points for quotation, not fixed catalogue limits. The selected spoke geometry, metal gauge, mirror thickness and mounting arrangement determine the final weight and workable diameter. Confirm the finished size from the outside tip of one ray to the opposite tip.
| Customisation point | Typical options for development | Production consideration |
|---|---|---|
| Overall diameter | Approximately 450–900 mm, subject to design review | Larger spans need review of frame stiffness, weight and mounting points. |
| Central mirror | Round mirror; roughly 3–5 mm glass options, depending on assembly | Thickness and backing affect recess depth, finished mass and retention design. |
| Radial frame | Formed or cut metal rays with a selected spoke count and profile | Fine, closely spaced rays may require more setup and careful finishing. |
| Surface and colour | Powder-coated colours or selected plated appearances | Custom colour matching needs an approved sample and may affect minimum order quantity. |
| Mounting and backing | Hanger position and backing arrangement to suit the design | Confirm the intended wall-fixing method and finished weight before release. |
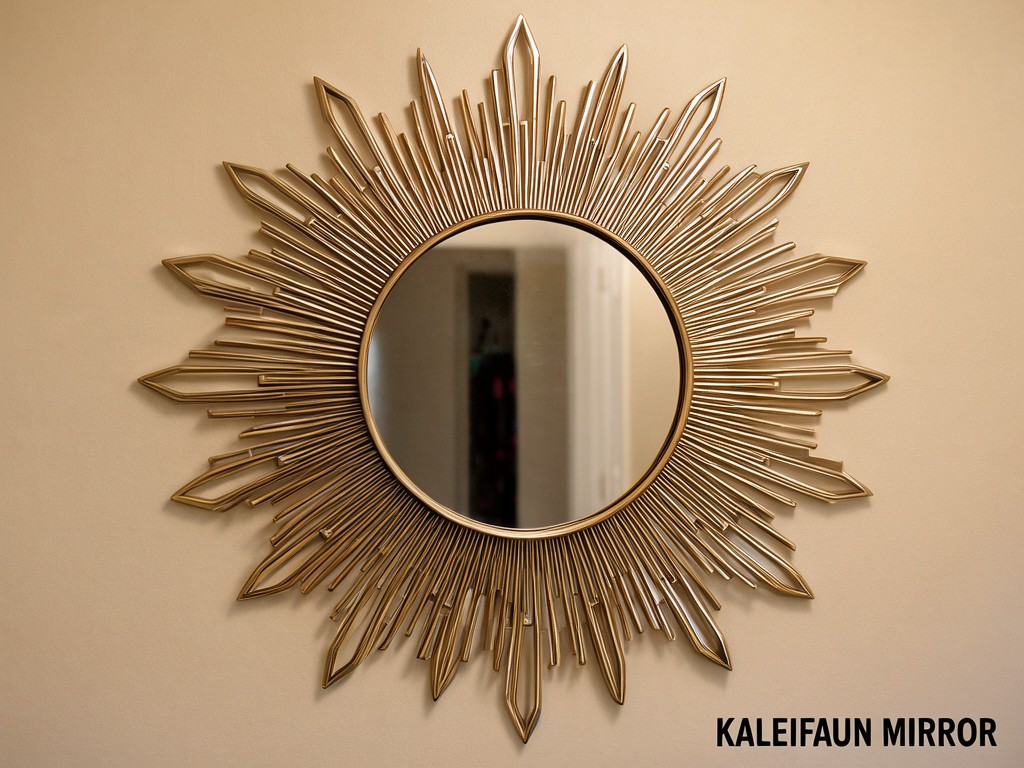
Deep rays, a wide outer span or a heavier mirror can exceed the practical limits of a light frame. In those cases, the design may need a revised section, additional support or a different mounting layout rather than a simple scale-up.
Who Uses It and Where It Matters
Home décor brands, furniture and gift wholesalers, and hospitality buyers select sunburst mirrors for feature walls where the radial outline is part of the room’s visual scheme. Retail displays often need a consistent face colour and spoke spacing across a range of sizes; hotel or restaurant projects may need the same finish repeated across multiple rooms and future replenishment orders.
Window-facing locations can expose finishes to prolonged sunlight, while kitchens, washrooms and spa-adjacent spaces may involve more frequent cleaning or airborne moisture. Specify those conditions before approving the finish. Harsh cleaners, chlorine vapour and abrasive cloths can mark coatings or plated surfaces, and the product should not be treated as suitable for wet or poolside installation without a finish and mounting review.
For routine care, a soft cloth and a cleaner suitable for mirror glass help limit scratches and residue. Keep liquid away from the mirror edge and rear assembly, where it can reach the reflective backing or metal joints.
OEM and ODM Programme Structure
An OEM programme can follow a buyer’s approved drawing, dimensions, finish and label requirements. ODM development is a better fit when the factory is asked to adapt a reference image or develop a new spoke arrangement. In either route, agreeing on the sample, revision status and approval owner early helps protect the planned launch date.
Buyer-Specified OEM
Provide a drawing or controlled sample with overall dimensions, mirror size, spoke profile, finish reference and mounting details. This route reduces design interpretation, but revisions after sample sign-off can require new setup or a revised production schedule.
Factory-Assisted ODM
Share reference images, target retail price, preferred diameter and finish direction. The factory can assess manufacturability and propose a sample route; custom geometry, colour matching or new stamping tooling can add cost and approval time.
For either programme, lock the approved artwork and finish reference before production materials are committed. If the launch date is fixed, set sample review and buyer-response dates alongside the order plan.
What Gets Checked Before Shipment
Inspection should compare finished units with the approved sample and specification, not just confirm that the mirror is present. Checks can cover outside diameter, spoke spacing, frame depth, mounting position and unit weight against the agreed tolerances. Visual review looks for coating skips, scratches, burrs, uneven colour, chipped glass and visible distortion in the reflection.
- Confirm the mirror sits securely in its retainers and has no movement under the agreed handling check.
- Review coating coverage around joins, ray edges and other areas where surface preparation can be difficult.
- Check finish colour against the approved physical sample under consistent viewing conditions.
- Agree any adhesion or corrosion exposure checks in advance; acceptance conditions depend on the specified finish and intended use.
If a buyer requires a particular cleaning or exposure assessment, define the cleaner, contact time and pass criteria before sampling. An unspecified “chemical-resistant” requirement is not enough to select or verify a finish.
Stock Availability and Reorder Planning
Sunburst mirrors are commonly produced to order because diameter, spoke geometry and finish vary by programme. Existing frame tooling or a repeat finish may shorten preparation, but neither confirms that a finished unit is in stock. Ask for current material and production status against the required ship window before setting a retail launch date.
For planned replenishment, retain the approved drawing revision, finish reference, sample record and inspection criteria. Forecasts help the factory plan metal, glass and finishing capacity; changes to colour, dimensions or quantity should be raised early because they can alter both cost and production timing.
Review Tooling Before You Commit
Send the target diameter, spoke layout, mirror specification, finish reference, order quantity and required launch date for a tooling review. Early review can identify geometry or finish choices that add cost or extend sample approval before they affect the production schedule.